An external thermal insulation composite system is only as good as its two thinnest layers: the 3–8 mm of adhesive that holds the insulation board to the wall and the 3–5 mm of base coat that carries the mesh and keeps rain out for 25 years. Both are polymer-modified dry mortars, and both pass or fail ETAG 004 / EAD 040083 on their additive package. This page sets out the Landercoll®, Accurate® and NOVASTAR® grades for each layer, the dosage ranges we start from, and the failures that European applicators report most often.
| Layer | Function | Critical requirements (EAD 040083-00-0404) | Additive priorities |
|---|---|---|---|
| Adhesive mortar | Bonds EPS, XPS, mineral wool or wood-fibre boards to masonry or concrete | Bond to substrate ≥ 0.25 N/mm²; bond to EPS ≥ 0.08 N/mm² or board failure; tested dry, wet and after 2 h/7 d re-drying | Water retention on absorbent masonry, wet-out of EPS skin, open time for board adjustment, sag resistance under board weight |
| Base coat (reinforcing render) | Embeds glass-fibre mesh, bridges cracks, resists impact and weather | Water absorption < 1 kg/m² after 24 h for base coat and complete render; hygrothermal cycling (heat–rain, heat–cold) without cracking or debonding; impact category I/II/III; freeze–thaw where required | Flexibility (crack bridging), hydrophobicity, adhesion to EPS/MW, pumpability for machine application |
| Finishing render / decorative coat (mineral) | Colour, texture, weather skin | Water absorption, vapour permeability, freeze–thaw | Workability, open time for floating, water repellency, efflorescence control |
The same cellulose ether grade can serve all three layers; the polymer powder and hydrophobic components change layer by layer.
Landercoll® cellulose ether. Every grade below carries EIFS / ETICS on its technical data sheet: K100H (“EIFS and standard tile adhesives”), K150 (“EIFS/EITCS, tile adhesives, skim coat”), K200 and K200H (“tile adhesives, EIFS/EITCS, skim coat”), K40H (“premium tile adhesives and EIFS”), EM40HT (“EIFS — surface mortar and adhesive mortar”), EM100H (“cement-based tile adhesives and EIFS”) and EM200 (“tile adhesives, EIFS/EITCS”). K75 and EM80 are the cement render grades used for mineral finishing coats. Viscosities are Brookfield RV, 2 % solution, 20 °C.
| Mortar | Grades (viscosity) | Starting dosage | Why |
|---|---|---|---|
| Adhesive mortar, hand-applied | K150 (55,000–65,000) · K200 (65,000–80,000) / EM200 (65,000–80,000) | 0.30–0.40 % | Water retention “very high” (K150) and sag resistance “excellent” (K200, EM200) for board weight on brick and AAC |
| Adhesive mortar, machine-applied | K100H (45,000–60,000) / EM100H (45,000–60,000) | 0.30–0.40 % | Pumpable viscosity with high water retention; EM100H sag resistance “excellent” |
| Base coat, hand and machine | K100H · K40H (20,000–24,000) / EM40HT (18,000–23,000) | 0.25–0.35 % | Smooth mesh embedding, no sag at 4–5 mm; EM40HT is the TDS grade for EIFS surface mortar |
| Base coat for Southern Europe / summer | EM40HT · EM100H (HEMC) | 0.30–0.40 % | Heat resistance “excellent” on the HEMC TDS versus “standard” for HPMC |
| Mineral finishing render | K75 (35,000–40,000) / EM80 (35,000–45,000) | 0.15–0.25 % | Cement render grades: float finish, texture stability |
Accurate® redispersible polymer powder
| Mortar | Grade family | Grades (TDS Tg / MFFT) | Starting dosage |
|---|---|---|---|
| Adhesive mortar to EPS/XPS | Rigid or semi-flexible VAE | 5011N (Tg 10 ± 5 °C / 4 °C; TDS: adhesive and surface mortar for EIFS), 4025N (Tg 0 °C / 1 °C; TDS: adhesive mortar for EIFS) | 2–3 % |
| Adhesive mortar to mineral wool / wood fibre | Semi-flexible | 4025N | 3–4 % |
| Base coat, standard (impact cat. III/II) | Flexible | 5045N (Tg −10 ± 5 °C / 0 °C; TDS lists EIFS), 9055E acrylic–silane (Tg −15 °C / 0 °C) | 3–5 % |
| Base coat, high impact (cat. I) or renovation on old render | Flexible + strong hydrophobic | 5045N + 8035H (TDS: adhesive & base-coat mortars, mineral renders) | 5–8 % total |
| Base coat with declared low water absorption | Hydrophobic | 8035H (strong hydrophobic effect), 8048H (very strong, instant-dissolving) | 3–5 % |
| Mineral finishing render | Semi-flexible or hydrophobic | 4025N, 8035H | 1–2 % |
NOVASTAR® specialty additives
Dosages are percentages of the total dry mix for laboratory starting points; the technical data sheets do not prescribe dosages. Verify against ETAG 004 / EAD 040083 test methods with your cement and sand.
| Symptom | Likely cause | Adjustment |
|---|---|---|
| Boards debond with clean EPS surface | Mortar skinned before the board was pressed; low polymer | K200H or EM40HT at 0.35–0.40 % for water retention; RDP ≥ 2.5 %; check EPS surface is dust-free and not UV-degraded |
| Boards slide after placement | Low sag resistance | 0.05 % ST3547; K200 / EM200 instead of K100H (sag resistance “excellent” on the TDS); reduce water |
| Cracks along mesh overlaps | Base coat too thin at overlap; rigid polymer | Minimum 3 mm cover over mesh; flexible 5045N / 9055E ≥ 3 %; 0.1 % PP fibre |
| Map cracking of base coat in summer | Fast water loss on EPS in sun | HEMC EM40HT or EM100H (heat resistance “excellent”); shade and mist-cure; fibre |
| Water uptake > 1 kg/m² at 24 h | No hydrophobic component; high w/c | SHP 0.3 %; hydrophobic RDP 8035H; lower water with ST3511 |
| Efflorescence on finishing render | Soluble salts carried by water movement | SHP 0.3–0.5 %; hydrophobic RDP; low-alkali cement |
| Pump blockage, pulsing output | Water retention drops under pump pressure; air | EM100H / EM40HT; defoamer P805; consistent water dosing |
| Freeze–thaw spalling of base coat | Low polymer, high air, water uptake | RDP ≥ 4 % flexible; SHP; defoamer |
| Biological growth, dark streaks | Surface stays wet | Hydrophobic additives; finishing render with lower water absorption |
Related guides: EIFS adhesive formulation guide · Improving bonding strength in EIFS adhesives · What is an EIFS system · 5 Common EIFS Adhesive Problems Seen on Site.
| Component | Adhesive mortar | Base coat |
|---|---|---|
| CEM I / CEM II 42.5 | 30–35 % | 25–30 % |
| Hydrated lime | 0–5 % | 3–5 % |
| Quartz sand 0.1–0.6 mm | 55–60 % | 55–60 % |
| Limestone filler / lightweight filler | 5–8 % | 5–10 % |
| Landercoll® cellulose ether | K150 0.35 % | EM40HT 0.30 % |
| Accurate® RDP | 4025N 2.5 % | 5045N 4 % |
| NOVASTAR® starch ether ST3511 | 0.05 % | 0.03 % |
| NOVASTAR® SHP75 / SHP80 | — | 0.3 % |
| PP fibre 6 mm | — | 0.1 % |
| NOVASTAR® defoamer P805 | — | 0.15 % |
Starting points only; the board type, substrate and target impact category determine the final polymer and hydrophobic dosage.
LANDU manufactures Landercoll® cellulose ethers, Accurate® polymer powders and NOVASTAR® additives in three plants in Shandong (75,000 t/year) and has supplied dry-mortar producers in Europe since 2011. All grades are REACH-compliant and produced under ISO 9001; batch certificates follow every shipment. Stock is held with partners in several European countries, including Greece, Spain and Italy, for call-offs below a container; factory lead time is 7–15 working days. Packaging per TDS: 25 kg bags with PE inner liner, 500–600 kg pallets for cellulose ether and 600–1,300 kg pallets for RDP, neutral or OEM bags on request. Our application laboratory runs pull-off tests on EPS and mineral wool, water absorption and freeze–thaw screening on customer formulations.
See LANDU’s production facilities, manufacturing processes and industrial additive portfolio.
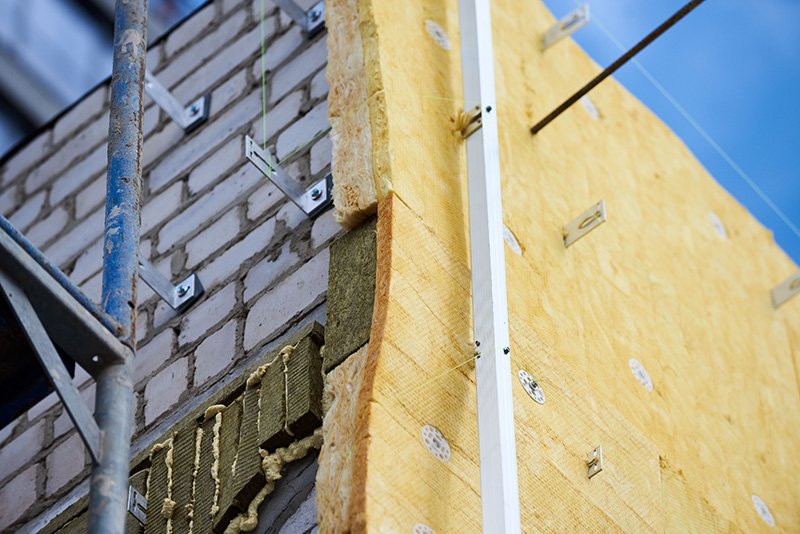
Review LANDU’s approach to raw-material inspection, process control, batch tracking and finished-product testing.
A Technical Data Sheet (TDS) describes the specifications and technical characteristics of a product grade. A Certificate of Analysis (COA) reports measured results for an identified production batch. Both documents support raw-material evaluation alongside application testing.
Contact LANDU about technical documents and batch-specific COA information for your selected material.
2–3 % for EPS and XPS boards, 3–4 % for mineral wool or wood-fibre boards, which have a more open surface. Accurate® 5011N and 4025N both list EIFS adhesive mortar on their technical data sheets. The target is board failure (cohesive failure in the insulation) in the ETAG 004 pull-off test rather than adhesive failure at the interface.
A flexible grade — Accurate® 5045N (Tg −10 ± 5 °C, MFFT 0 °C) or the acrylic–silane 9055E (Tg −15 °C) — at 3–5 %. It provides the crack bridging across board joints and the impact resistance the EAD requires. Add the strongly hydrophobic 8035H or 0.3 % SHP when a low water-absorption class is declared.
Both are used. The HEMC data sheets (EM40HT, EM100H, EM200) rate heat resistance "excellent", so HEMC is preferred for machine application and for sites above 30–35 °C; HPMC (K100H, K150, K200, K200H) is the economical choice for hand-applied adhesive in temperate climates.
Three levers: 0.2–0.5 % NOVASTAR® SHP, a hydrophobic RDP grade (8035H or 8048H), and lower water demand through 0.03–0.05 % starch ether ST3511. Most base coats reach the threshold with SHP at 0.3 % plus 4 % flexible RDP.
Indirectly. Good water retention keeps the mortar surface wet long enough to wet out the EPS skin before the board is pressed; a mortar that skins in 10 minutes bonds poorly however much polymer it contains. Open time, controlled by the cellulose ether grade, is the first thing to check in a debonding case — K200H and EM40HT are the grades with the highest water retention on the TDS.
We supply technical data sheets, REACH documentation and application test reports from our laboratory (pull-off on EPS/MW, water absorption, freeze–thaw screening). The formal ETA is issued for the system holder's complete kit; we support the formulation work that leads to it.
A cellulose ether for water retention and sag resistance (Landercoll® K150, K200 or EM200 at 0.30–0.40 % in the adhesive; K100H, K40H or EM40HT at 0.25–0.35 % in the base coat), a redispersible polymer powder for adhesion to the board and crack bridging in the base coat (Accurate™ 5011N or 4025N at 2–3 % in the adhesive; 5045N or 9055E at 3–5 % in the base coat), and, as the system requires, a starch ether for sag (ST3511), a hydrophobic powder or 8035H for declared water absorption, PP fibre and a defoamer.
The polymer film from the RDP is what bonds a cement mortar to EPS or mineral wool (cement paste alone has almost no adhesion to polystyrene) and what lets a 3–5 mm base coat follow the thermal movement of the board without cracking. Below about 2 % the adhesive fails at the board face; above 4–5 % cost rises faster than performance. The mesh carries the tensile load; the RDP keeps the base coat attached and flexible around it.
Yes: insulation boards bonded and, where required, dowelled to the wall, a mesh-reinforced base coat and a finish. "EIFS" is the North American term, "ETICS" the European one. In Europe the system is assessed under EAD 040083 (formerly ETAG 004), which is where the bond, water absorption and impact requirements on this page come from. System overview: What is an EIFS system?.
North American terms. A PB system uses a thin, polymer-rich (acrylic-based) base coat of about 1.6 mm (1/16 in) over the insulation; a PM system uses a thicker cementitious base coat, typically 5–13 mm (3/16–1/2 in), modified with polymer and usually applied over a mechanically fixed board. The dry-mix adhesives and base coats on this page are the PM type and the European ETICS type: cement-based, polymer-modified with Accurate™ RDP and given their working properties by Landercoll® cellulose ether. Confirm the system class and its requirements in the system specification before selecting grades.
Yes, and "2-in-1" mortars are common: in practice the base-coat recipe (K100H or EM100H at 0.30–0.40 %, 3–4 % 4025N or 5045N) is also used for bonding. The cost is extra polymer in the adhesive layer, where 2–3 % would do. Qualify the two uses separately: bond to the board and to the substrate for the adhesive; water absorption, impact and crack bridging for the base coat.
We return grade recommendations and dosages within two working days and ship samples free of charge.
LANDU — Committed to Every Gram.